
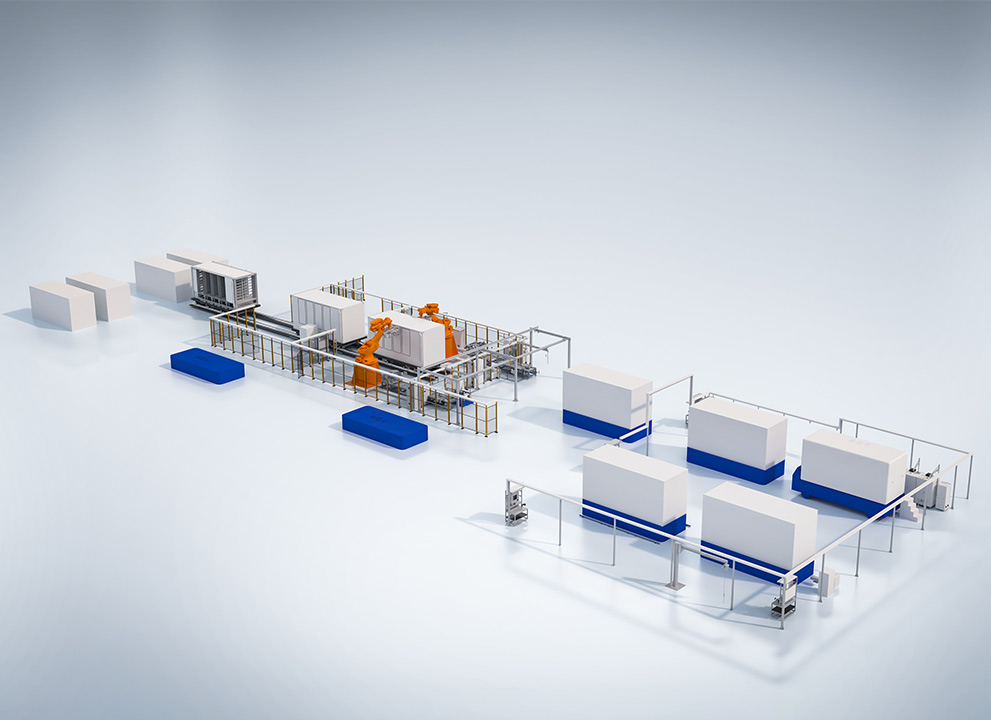
Problem focus: Why manual and fragmented lines fail battery quality targets
Production teams face rising rejection rates, unpredictable throughput, and safety incidents because manual handling and disjointed control systems introduce variation at every handoff. That variation multiplies across processes—electrode stacking, cell welding, electrolyte filling—so a single alignment or torque drift becomes a batch-level fault. Many facilities address symptoms with overtime or inspection, but those responses increase cost without reducing root causes; targeted battery manufacturing automation stops the amplification by controlling the inputs where defects originate.

Root causes and the cascade of effects
Cause: inconsistent fixturing, inadequate sensing, and human variability at critical joins. Effect: micro-misalignment that leads to internal shorting or capacity loss weeks after shipment. Cause: fragmented data flows and manual traceability. Effect: long recall investigations and lost production time. Cause: equipment chosen for speed rather than compatibility. Effect: integration friction that triggers downtime and hidden cost overruns. One practical anchor for scale and impact is the Tesla Gigafactory in Nevada, where high-volume cell assembly revealed how small process shifts scale into major supply risks.

Priorities that directly change outcomes
Addressing the problems means matching controls to failure modes. Prioritize these, in order, and expect the listed outcomes:
– Tight mechanical control: precise end-of-arm tooling and repeatable fixturing reduce alignment defects; outcome—fewer latent failures. – Inline sensing (vision, force, electrical): immediate detection of anomalies; outcome—rejects flagged before assembly. – Closed-loop servo and torque control: consistent welds and fasteners; outcome—repeatable electrical and mechanical joins. – MES and traceability: automated lot IDs and parameter logs; outcome—minutes instead of weeks to isolate batches. – Safety interlocks and soft robotics: lower injury rates and gentler cell handling; outcome—reduced downtime and warranty exposure. These priorities cause a direct drop in rework hours and increase first-pass yield when implemented in sequence rather than in isolation.
Where battery assembly automation fits into the line
Choose automation where human variability creates the largest failures. For example, automated electrode stacking, laser tab welding, and controlled electrolyte dosing remove repeatable risk. The best gains come from pairing hardware with process-aware software—vision that not only rejects but feeds correction parameters, robots that adjust force based on sensor input, and MES rules that lock out suspect lots. Integrating battery assembly automation at these touchpoints converts variable inputs into predictable outputs.
Implementation roadmap: cause-to-solution steps and common pitfalls
Step 1 — Map failure modes to line stations. You must prove which station causes the majority of defects. Step 2 — Pilot a closed-loop fix on that station with measurable metrics: defect rate, cycle time, and MTTR. Step 3 — Scale horizontally only after metrics stabilize. Common mistakes are skipping the pilot, over-automating low-impact stations, and ignoring maintenance bandwidth. Each mistake causes schedule slippage and eats ROI. Assign a cross-functional owner—production, controls, and maintenance—to keep cause–effect accountability tight.
Evaluating approaches: in-house, turnkey, or hybrid
In-house development causes strong tailoring but often delays launch because teams under-estimate controls complexity. Turnkey solutions reduce start-up risk but can cause vendor lock-in and mismatches with existing MES. Hybrid approaches let you control critical intellectual property (cell handling, test algorithms) while outsourcing standard modules (robot cells, vision stacks). Choose the approach that minimizes the biggest cause of failure you identified earlier; that choice drives time to stable output and cost exposure.
Practical metrics and governance to measure effect
Track a short list of leading indicators that show cause reduction: first-pass yield, process capability (Cp/Cpk) for critical dimensions, defect escape rate to final test, and mean time to diagnose a batch issue. Weekly dashboards should link these indicators to specific line changes so teams see the causal chain. Regular reviews that include operators reveal latent process drift before defects spike.
Common technical pitfalls and how their causes are fixed
Pitfall: vision rejects that vary with lighting. Fix: controlled lighting enclosures and standardized calibration routines to remove environmental cause. Pitfall: robot path drift after maintenance. Fix: homing routines and fixture verification that catch drift before production. Pitfall: MES records that are incomplete. Fix: automated data capture at handoffs so root-cause analysis uses reliable inputs rather than recollection.
Concluding synthesis
When problems are mapped to their causes and controls are applied where they interrupt the failure chain, outcomes become predictable: lower rework, stable throughput, and safer handling. The path that delivers those outcomes combines focused automation, tight sensing, and governance that ties changes to measurable effects. Operators and engineers gain clarity, and decision-makers see investment payback in reduced defects and faster investigations—an approach I’ve overseen on multi-line rollouts and one that aligns naturally with the services and solutions offered by FHS.